all search
Tel: 0386-311-66695955, +86 18631137373
Factory Address: No.29-11 Jinyu Avenue, Zanhuang Economic Development Zone, Shijiazhuang City, Hebei Province, P.R.China
Office Address: 14th Floor, East Wing, Business Building 6, Xuhui Zhongrui Mansion, No.281 South Jianshe Avenue, Shijiazhuang City, Hebei Province
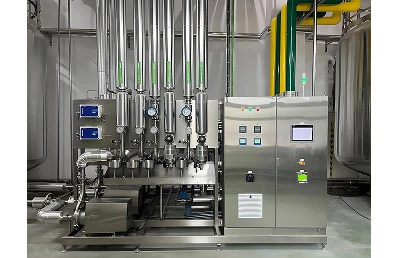
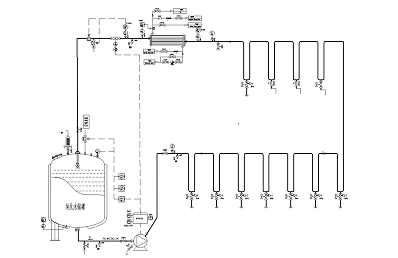
Fully automatic liquid dispensing systemIt is a core intelligent equipment in the pharmaceutical, biopharmaceutical, food and beverage, and fine chemical industries, relying on functions such as automated feeding, constant temperature ratio, homogeneous stirring, CIP online cleaning, SIP in-situ sterilization, etc., to achieve standardized preparation of drug solutions, excipient solutions, and process fluids. The operational accuracy, cleanliness level, and production stability of the entire system are closely related to the quality of pipeline docking and installation.
The fully automatic liquid dispensing system includes various types of pipelines such as material conveying pipelines, purified water pipelines, cleaning pipelines, steam pipelines, and sewage pipelines. Unlike ordinary industrial pipelines, its docking and installation require higher requirements for cleanliness, sealing, no dead corners, washability, and traceability. If the pipeline connection is not standardized, it is easy to encounter problems such as material residue, cleaning blind spots, medium leakage, cross contamination, unstable pressure, and ratio deviation, which directly affect the consistency of product batches and the effectiveness of workshop GMP acceptance. To assist construction and operation personnel in standardizing construction, this article provides a detailed overview of the core precautions and compliance standards for the installation of fully automatic liquid dispensing system pipelines.
1、 Precautions for pipeline material selection: Suitable for clean process conditions
The material of the pipeline is the basis for ensuring the cleanliness of the liquid preparation medium and avoiding secondary pollution. The pipeline of the fully automatic liquid preparation system that comes into contact with the material and purified water complies with industry clean production and pharmacopoeia related specifications, eliminating the problems of precipitation, corrosion, and pollution caused by non-standard materials.
For process pipelines that come into direct contact with liquid medicine, ingredient solutions, and purified water, 316L sanitary grade stainless steel pipes are preferred. The inner wall of the pipe is finely polished to meet the surface roughness standard, and the inner wall is smooth without pores, cracks, or slag inclusions. It is not easy to adhere to viscous materials, powder impurities, and can adapt to repeated high-temperature sterilization and acid-base cleaning conditions. The material stability is good. The auxiliary pipelines and sewage pipelines for non-contact materials can be made of 304 sanitary grade stainless steel material, which meets the basic requirements of corrosion resistance and easy cleaning.
The sealing gaskets, O-rings, and diaphragm seals used for pipeline matching should be made of pharmaceutical grade compliant materials, such as EPDM, PTFE, medical silicone rubber, etc., which have the characteristics of high and low temperature resistance, acid and alkali resistance, no precipitation, and can be repeatedly sterilized. They are suitable for CIP cleaning and SIP high-temperature sterilization conditions to avoid aging and detachment of seals, as well as contamination of materials caused by medium precipitation. All pipes and fittings must have complete material certification documents to meet GMP traceability requirements.
2、 Precautions for pipeline layout design: eliminate cleaning dead corners and material residues
The fully automatic liquid preparation system supports automated cleaning and sterilization functions, and the rationality of pipeline layout directly determines the landing effect of CIP and SIP processes. It is the core control link for pipeline docking and installation, and must strictly follow the design principles of no dead corners, easy emptying, and easy cleaning.
The overall pipeline route should be simple and orderly, following the principle of short paths and minimal connections. The pipeline length should be planned reasonably, and unnecessary elbow, tee, variable diameter, blind pipe and other connection structures should be minimized as much as possible. The length of blind pipes should be strictly controlled within the industry compliance range to avoid fluid retention areas, prevent long-term accumulation, drying and deterioration of materials, breed microorganisms, and form cleaning blind spots.
All process pipelines must have a reasonable drainage slope, with reserved inclination angles according to the flow direction of the medium, to ensure that after production and cleaning are completed, the materials and cleaning wastewater in the pipeline can be naturally and completely drained without water accumulation or material residue, reducing residual pollution hazards from the source. Pipeline layout should avoid areas with strong equipment vibration and high temperature heat sources to reduce interface looseness and pipeline fatigue aging caused by long-term resonance.
Different functional pipelines need to be arranged in different zones. Material pipelines, pure water pipelines, steam pipelines, and sewage pipelines should be separated in an orderly manner to avoid cross interference and heat interference between pipelines. At the same time, sufficient space for maintenance and disassembly should be reserved to facilitate later pipeline maintenance, accessory replacement, and deep cleaning.
3、 Precautions for hygiene grade docking process: Ensure a sealed, clean and no blind spots
Fully automatic liquid dispensing systems are commonly used in high-purity production scenarios. Ordinary rough connection methods are prohibited for pipeline docking, and sanitary docking processes must be carried out throughout the entire process, taking into account sealing, flatness, and cleanability.
The docking position between the tank interface, equipment port, and pipeline should prioritize the use of sanitary grade quick release clamps and sanitary flange connections, which are easy to disassemble and tightly sealed. The inner wall of the interface should be flat without protrusions or gaps, and there should be no dead corners for dirt and grime accumulation. It is suitable for daily disassembly, cleaning, and regular maintenance. Core material conveying pipelines and pure water pipelines are prohibited from using ordinary threaded connections, as threaded gaps are prone to residual materials and dirt accumulation, which does not comply with GMP cleanliness standards.
The on-site welding operation of pipelines requires the use of clean argon arc welding technology, with full and uniform welds, no porosity, no slag inclusion, and no cracks. After welding is completed, the internal and external welds are finely polished and polished to ensure that the inner wall of the pipeline is smooth and consistent with the pipe body, avoiding rough welds, hanging materials, and dust accumulation. Welding operations should be carried out in a dust-free construction environment, and welding slag and debris should be promptly cleaned to prevent impurities from remaining inside the pipeline.
When connecting pipelines, it is necessary to ensure that the interfaces are concentric, horizontally aligned, without offset or inclination, to avoid local gaps, fluid turbulence, material wall hanging and other problems caused by interface misalignment, and to ensure smooth medium transportation and good pipeline sealing.
4、 Precautions for sealing installation: Avoid leakage and external pollution
The pipeline of the fully automatic liquid dispensing system needs to withstand alternating changes in medium pressure and temperature for a long time, and the quality of sealing installation directly affects the stability and cleanliness of the system operation. It is necessary to strictly control the installation details of each sealing point.
Before installing the sealing components, it is necessary to complete an inspection to remove gaskets and sealing rings that are deformed, cracked, aged, damaged, or stained. At the same time, the flange end face, clamp contact surface, and sealing groove should be cleaned to remove dust, oil stains, and impurities, ensuring that the sealing fitting surface is clean and flat, and providing the basic conditions for a tight fit.
The sealing ring should be installed in the center and aligned without offset, compression, or leakage. The flange and clamp fastening should follow the principle of symmetrical and staged locking, with uniform force to avoid interface deformation, sealing failure, or micro leakage gaps caused by uneven force due to excessive single point fastening force. After the installation of all sealing points is completed, it is necessary to check the fitting gaps one by one to ensure that they are tight and not loose.
For steam and high-temperature cleaning pipelines, it is necessary to select sealing accessories that are suitable for temperature resistance levels, adapt to alternating cold and hot working conditions, offset the changes in sealing clearance caused by thermal expansion and contraction, avoid interface leakage, air intake and other problems under high-temperature working conditions, and ensure the sealing performance of pipelines during alternating high and low temperature operation.
5、 Precautions for installation of valves and auxiliary accessories: Adapt to automation process logic
The fully automatic liquid dispensing system relies on auxiliary components such as valves, filters, sensors, and exhaust valves to achieve automated linkage control. Whether the installation position and direction of the components are standardized directly affects the accuracy of liquid dispensing, cleaning effect, and system linkage stability.
Sanitary grade diaphragm valves, ball valves, and other self-control valves must be installed strictly according to the flow direction of the medium, with the opening and closing directions matching the system control logic. The installation position should be convenient for daily operation, observation, and maintenance, ensuring flexible opening and closing, reliable sealing, and no jamming, and suitable for automated program control. Reverse installation and inclined installation are prohibited to avoid problems such as medium backflow and control failure.
An exhaust device should be installed at the high point of the pipeline to promptly remove the accumulated air inside the pipeline, eliminate air blockage and bubble problems, and ensure uniform and stable medium transportation and water flow cleaning; A drainage and emptying interface should be installed at the low point of the pipeline to facilitate the emptying of residual liquid and flushing of impurities, without any dead corners at the bottom. The material pipeline and pure water pipeline need to be equipped with filtering accessories to intercept impurities and protect the sensing elements and the clean environment inside the tank.
Flow, pressure, temperature and other sensing accessories need to be installed at standard measuring points, avoiding pipeline bends and turbulent flow areas, ensuring accurate data collection, ensuring accurate system automation proportioning, temperature control, and pressure regulation parameters, and avoiding process abnormalities caused by data deviation.
6、 Dust free construction and cleaning protection precautions: eliminate secondary pollution
Fully automatic liquid dispensing systems are often installed in pharmaceutical and food clean rooms. Pipeline docking construction must strictly follow clean construction standards, strictly control construction pollution sources, and avoid construction residues affecting workshop cleanliness and material safety.
All pipes and fittings must undergo dust removal, wiping, and cleaning before entering the site to remove impurities such as factory dust, oil stains, and iron filings. They should be stored in a dry and sealed manner, and it is prohibited to bring contaminated materials into the clean work area. Construction tools need to be cleaned and disinfected in advance, and operators should wear dust-free protective equipment throughout the process, strictly following the construction standards of the dust-free workshop.
Dust prevention measures should be taken for pipeline cutting, welding, and drilling operations, and debris, welding slag, and dust generated should be cleaned up in a timely manner. Open dust operations are prohibited in clean areas. After the completion of the single section pipeline docking, the pipe mouth should be immediately sealed to prevent workshop dust, water vapor, and debris from entering the interior of the pipeline and avoid secondary pollution.
After the completion of the entire pipeline construction, all pipelines need to be subjected to multi-stage blowing, flushing, and disinfection to remove residual impurities from the construction. Only after confirming that the interior of the pipeline is clean and free of residue can it enter the commissioning stage to ensure that the cleanliness of subsequent production materials meets the standard.
7、 Precautions for pressure testing, leak detection, and commissioning acceptance: Ensure system stability and compliance
After the completion of pipeline docking and installation, direct production and use are strictly prohibited. Through standardized pressure testing, leak detection, debugging and acceptance, hidden dangers are investigated to ensure the compliance and usability of the pipeline system.
Conduct air pressure or water pressure sealing tests according to equipment process standards, observe the specified duration of pressure stabilization, inspect all connection points such as pipeline welds, clamp interfaces, flanges, valves, etc., confirm that there are no leaks, pressure drops, pipeline deformations, air leaks, etc., and ensure that the sealing performance of the entire pipeline meets the standard. After the pressure test is completed, drain the accumulated water and residual medium in the pipe to avoid the growth of microorganisms and the formation of scale in the accumulated water.
During the acceptance stage, it is necessary to verify the slope of the pipeline, the emptying effect, the layout direction, and the standardization of accessory installation, to confirm that there are no cleaning dead corners, no residual blind spots, and smooth transportation. Subsequently, a no-load and material linkage trial run was carried out to test the stability of the pipeline medium conveying pressure, no resonance or abnormal noise, and no material retention. The automatic start stop, cleaning, and sterilization process linkage was normal.
After passing the acceptance inspection, retain traceability information such as pressure testing records, installation records, debugging data, cleaning records, etc., to meet the requirements of workshop GMP compliance management and audit tracking.
8、 Precautions for later operation and maintenance: Suitable for long-term clean production
During the pipeline docking and installation phase, it is necessary to take into account the later maintenance and cleaning needs, reduce the difficulty of subsequent maintenance and cleaning from the layout and structure, and ensure the long-term stable operation of the system.
Easy to wear and tear seals, valves, filter cartridges, and other accessories should be installed with sufficient space for disassembly and assembly. Replacement and maintenance can be completed without the need for extensive disassembly of pipelines, reducing the risk of pollution and time loss caused by disassembly and assembly operations. The overall pipeline layout needs to be fully adapted to the CIP online cleaning process of the equipment, ensuring that the cleaning water flow and steam fully cover the inner walls and interface positions of the pipeline, without any cleaning blind spots, and guaranteeing long-term production cleanliness stability.
At the same time, it is necessary to reserve pipeline inspection points for regular leak detection, parameter calibration, and pipeline cleaning verification in the later stage, to continuously ensure the sealing, cleanliness, and operational accuracy of the fully automatic liquid dispensing system pipeline.
Summary
Fully automatic liquid dispensing systemThe core considerations for pipeline docking installation are mainly reflected in seven core dimensions: clean material selection, no dead angle pipeline layout, sanitary docking process, refined sealing installation, compliant valve layout, dust-free construction control, and pressure testing compliance acceptance. Compared to ordinary industrial pipeline installation, fully automatic liquid dispensing system pipelines pay more attention to cleanliness, emptying, sealing, and verifiability. All installation details revolve around avoiding material residue, eliminating cross contamination, and ensuring that automated processes comply with GMP compliance standards. Standardizing the installation of pipeline connections can effectively improve the accuracy of liquid dispensing, cleaning and sterilization effects, and operational stability of fully automatic liquid dispensing systems, reduce equipment failures and material losses, and meet the high cleanliness and automation production needs of industries such as pharmaceuticals, food, and fine chemicals.